A satellite unit may work perfectly on a test bench, then develop problems after installation on the spacecraft: low supply voltage, fluctuating temperature readings, intermittent bus errors or higher-than-expected radio-frequency (RF) losses. The fault may lie in the cable connecting the unit.
A cable is rarely a transparent path between two devices. It has resistance, inductance, capacitance, thermal resistance, mass and mechanical stiffness. It must also withstand vacuum, temperature cycling, vibration, radiation and bending during assembly. Change what the cable carries, and the selection criteria change with it.
Satellite cables should first be classified by their transmission function and installation environment. Engineers can then choose the conductor, insulation, twisting, shielding, jacket and termination method. A quality designation describes how a product is manufactured, qualified, inspected and traced; it cannot replace analysis of voltage drop, impedance, shielding, bending or the space environment.
1. Wire, Cable and Harness Are Different Levels of Assembly
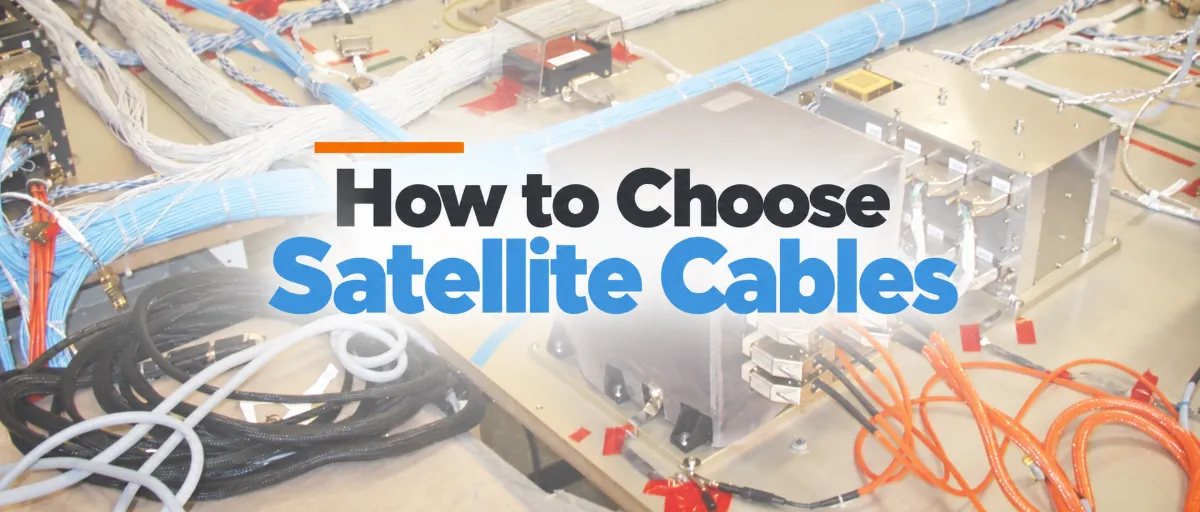
At its simplest, a wire consists of a metal conductor and insulation. Several insulated wires may be twisted together and combined with shielding, fillers or an outer jacket to form a cable. A harness brings wires and cables together with connectors, branches, identification, protective sleeving and fasteners according to the spacecraft’s interfaces.
Each level introduces different quality concerns. A wire must meet requirements for its conductor, insulation and finished properties. A cable may also need controlled impedance, crosstalk, shielding and construction. Harness production adds stripping, crimping, soldering, shield termination, tying, routing and connector retention. Even if every spool of wire passes inspection, a poorly assembled harness can still suffer broken strands, unreliable contacts, damaged insulation or electromagnetic compatibility problems.
2. What the Line Carries Determines What It Needs
The first selection question is not whether a wire is “space grade.” It is what the line must carry. A heater supply and a weak temperature-sensor signal can have similar voltages but very different design priorities.
Power Lines: Calculate Voltage Drop and Heating First
Power lines deliver energy to spacecraft units, heaters, motors and actuators. Selection depends on maximum continuous current, peak current, allowable voltage drop, operating temperature, routing in bundles and duty cycle. An undersized conductor raises resistance, reducing the voltage at the load and turning more energy into heat along the line.
ΔU = I × R Ploss = I² × R
Here, ΔU is the voltage drop, I is current, and R must include the outgoing and return conductors as well as relevant contact resistance. Conductor resistance also changes with temperature.
Consider a 28 V heater drawing 4 A through a cable with a one-way length of 3 m. If the candidate wire has a resistance of 20 mΩ/m at the calculation temperature, its 6 m round-trip conductor length has a resistance of about 0.12 Ω. The wire alone would produce a 0.48 V drop and dissipate about 1.92 W. Connector resistance, branch points and temperature-driven changes in resistance must then be added. The example does not prescribe a wire gauge; it shows why a current rating alone is insufficient.
Vacuum provides no air convection, while adjacent wires in a bundle can heat one another. Allowable current is therefore not a fixed property independent of installation. It must be assessed against insulation temperature limits, bundle size, attachment methods, heat conduction into nearby structures and worst-case thermal conditions. Current-carrying tables for exposed wiring on the ground cannot simply be copied into a spacecraft design.
Wire size must also work with fuses, current limiters or electronic protection. Following a fault, the affected branch should be isolated before the wire, termination or connector suffers unacceptable thermal damage.
Low-Level Measurement Lines: Protect the Signal
Temperature, current and pressure sensors may produce very small signals. Wire resistance, loop area, electromagnetic coupling and the treatment of the reference ground can then affect the measurement itself. Common approaches include twisted pairs, shielding where needed, and physical separation from switching supplies and high-current pulse lines.
Resistance sensors such as platinum resistance thermometers may use three- or four-wire connections to reduce measurement error caused by lead resistance. Those connections address a specific measurement error; they are not a general interference remedy.
Twisting exposes the two conductors to more similar external interference while reducing loop area. A shield provides a controlled path for coupled currents. Its termination must be chosen according to signal frequency, the common-mode environment, the equipment grounding scheme and shield construction. Low-frequency measurements may require particular care to avoid ground loops; at high frequencies, shield continuity and low-impedance termination become more important. The choice cannot be reduced to a universal rule of grounding one end or both ends.
Digital Buses: Fast Edges Require Transmission-Line Design
Data rate alone does not determine whether a digital cable must be treated as a transmission line. Engineers must also compare signal rise and fall times with propagation delay through the cable. Once that delay is significant relative to the edge time, continuity checks are insufficient. Differential impedance, termination, topology, stub length, skew and crosstalk can all alter the waveform at the receiver. Wiring tolerated by a slow switching signal may cause reflections and errors on a bus with fast edges.
CAN, RS-422, MIL-STD-1553B and SpaceWire interfaces each have their own physical-layer and network requirements. SpaceWire, for example, addresses cable construction, differential impedance, insertion loss and skew as well as its differential signals.[11] The cable, connectors, branches and terminations must be verified as one link.
RF Coaxial Cable: Impedance Continuity Matters More Than Simple Continuity
A coaxial cable uses an inner conductor, dielectric and outer conductor to create a controlled RF structure. Many systems use 50 Ω interfaces, but link performance also depends on insertion loss across the operating band, standing-wave ratio, shielding effectiveness, power handling, phase stability over temperature and connector termination. A tight bend, crushed outer conductor or contamination introduced during assembly can change local impedance.
Flexible coaxial cable is easier to route. Semi-rigid coaxial cable generally offers greater control over geometry, shield continuity and repeatable installation, but demands more careful forming, assembly and repair. Selection should start with the complete RF link budget, including cable length, connector count, bend path and operating temperature.
High-Voltage and Special-Purpose Lines: Thicker Insulation Is Not a Complete Solution
High-voltage supplies, electric propulsion systems and pulsed loads call for attention to rated voltage, insulation thickness, creepage distance, electric-field concentration, partial discharge and surface contamination. Gas breakdown depends on gas type, pressure p and electrode spacing d. Paschen’s law describes how breakdown voltage varies with p × d, including a region where breakdown is more likely. A spacecraft passes through changing low-pressure conditions during ascent, so passing a withstand-voltage test at ordinary atmospheric pressure does not establish that discharge cannot occur throughout ascent.[12]
Gas breakdown generally becomes less likely in high vacuum. Surface flashover, field concentration where metal, insulation and vacuum meet, outgassing and contamination still require separate attention. High-voltage cables must be designed together with connectors, feedthroughs, clamps and clearances inside the equipment. Increasing insulation thickness alone will not remove concentrated fields at terminations or prevent surface discharge. High-power RF equipment may also face multipactor, which has its own design and test methods.[13]
Moving and External Lines: Mechanical and Environmental Demands Take the Lead
Cables crossing a solar-array joint, antenna mechanism or other moving interface must be assessed for minimum bend radius, repeated-flex life, control of the bend location and strain relief. A cable that meets electrical requirements in a static installation may develop conductor fatigue or cracked insulation under repeated movement.
External cables face wider temperature cycles, ultraviolet exposure and radiation. On exposed leading surfaces in low Earth orbit, polymers may also need protection against atomic oxygen. Coverings, shielding by surrounding structures, material choice and routing can reduce exposure. Optical fiber offers high bandwidth and electromagnetic isolation, but its terminations, bend losses and radiation-induced attenuation require separate evaluation.
3. Materials and Construction Must Follow the Operating Conditions
The conductor is a primary determinant of resistance and mass. Silver-plated copper, nickel-plated copper and copper-alloy products involve different trade-offs in conductivity, temperature capability, strength, termination processes and long-term storage.
For silver-plated copper, moisture and plating damage must be controlled during manufacturing, assembly and ground storage to prevent corrosion at defects in the copper–silver interface, commonly called “red plague.” This is primarily a processing and storage concern involving moisture, oxygen and interface defects; it is not caused by vacuum in orbit.[14] Aluminum alloy and copper-clad aluminum can save mass, but resistance, mechanical properties, joining methods and galvanic compatibility must be reassessed. GB/T 35852—2018 specifies conductor dimensions and characteristics for aircraft cables and aerospace applications, while GB/T 42043—2022 addresses aluminum-alloy and copper-clad aluminum conductors.[2][3] A Chinese study of a geostationary communications satellite likewise found that reducing conductor cross-section and insulation mass had to be validated alongside connections, tying and routing protection.[16]
Insulation does more than set a temperature limit. PTFE, FEP, ETFE, cross-linked ETFE and composite-tape insulation differ in mass, abrasion resistance, flexibility, processability, outgassing, radiation response and arc-tracking behavior. GJB 773B—2015 is the general specification for fluoropolymer-insulated aerospace wires and cables; individual products must also meet the applicable detailed specifications and procurement documents.[1] The same material name does not guarantee the same insulation thickness, manufacturing process or finished performance.
More shielding is not automatically better. Braid coverage, overlap, continuity through transitions, grounding points and backshell design affect shielding performance while adding mass and bending stiffness. Electromagnetic compatibility design should classify circuits by their emissions and susceptibility. ECSS standards likewise call for circuit classification according to electrical characteristics and sensitivity, with separation or segregation of harness categories as appropriate.[10]
4. From Requirements to a Cable Part Number
First, define the interface fully. Record whichever parameters apply: voltage, current, frequency, signal amplitude, source and load characteristics, allowable voltage drop, noise budget, bit-error rate or RF loss. “28 V power line” or “bus cable” is not a complete selection requirement.
Second, establish the cable’s location. Will it run inside a unit, between internal panels, across spacecraft sections, through a moving mechanism or outside the spacecraft? Which heat sources, sharp edges, openings and connector-access areas will it encounter? Can it run parallel to high-current wiring? Three-dimensional spacecraft harness design can bring bend radius, pass-through openings, mating clearance, functional segregation and assembly sequence into a single review.[15]
Third, perform electrical, thermal, EMC and mechanical analyses together. Calculate voltage drop and heating for power lines; check impedance and topology for digital lines; build an RF link budget; examine insulation along the full high-voltage path; and evaluate life and motion envelopes for moving cables. Use those results to choose the conductor, insulation, shielding, jacket and connectors.
Fourth, check the product specification and supply status. Confirm that the part number covers the required wire size, temperature, rated voltage and construction. Review the manufacturer, production line, qualification status, delivery lot and change history. Finally, use samples and system-level tests to show that the design works at its actual interfaces.
5. What Does Cable “Quality Grade” Mean?
Some electronic-component categories use designations such as S, JY and K to indicate quality or assurance levels. There is no single ranking of those letters that can simply be applied to every wire and cable. For cables, more useful questions are: Which general and detailed specifications apply? What is the exact construction? Is the manufacturer and production line approved? What consistency checks were performed on the delivered lot? Can its materials and manufacturing history be traced?
GJB 773B—2015 covers materials, construction, performance and quality assurance for fluoropolymer-insulated aerospace wires and cables. Codes describing a conductor, plating, insulation or jacket identify construction; they do not, by themselves, form a lowest-to-highest quality scale. Procurement must specify the detailed specification, product part number and ordering requirements. NASA’s EEE-INST-002 likewise treats wire and cable as a distinct category, with provisions for selection, screening, qualification and derating.[6]
Assurance effort should also reflect mission risk and the importance of the equipment. GB/T 46556—2025 addresses application levels as part of a selection and assurance strategy tied to mission risk, while GB/T 46560—2025 concerns process control systems.[4][5] An application level is not an immutable property stamped onto a spool. A critical installation generally calls for stronger evidence of qualification, lot consistency, change control, retesting and traceability. Other qualified sources may be considered where risk permits, but the mission environment, connector compatibility and termination processes still need verification.
Cable quality requires at least four kinds of evidence: product specification and qualification status, delivered-lot consistency, suitability for the actual operating conditions, and harness workmanship and verification. A label saying “aerospace” or “space grade” is not enough to select a cable.
6. Why a Harness Made From Qualified Wire Still Needs Testing
Turning wire from a spool into a harness involves cutting, stripping, crimping or soldering, preparing shields, forming branches, marking, tying and installation. Each step can damage conductors or insulation. Nicked strands, uncontrolled crimp height, discontinuous shield treatment or missing strain relief at a branch can become intermittent faults after vibration and thermal cycling.
Crimping is particularly dependent on process control. Contacts, wire gauges, plating and crimp tools must be compatible. Tool condition, operator qualification, crimp parameters and pull-test verification must be controlled. NASA-STD-8739.4A and ECSS-Q-ST-70-26C set manufacturing and quality requirements for high-reliability wiring and crimped connections. ECSS-Q-ST-20-30C, published in 2025, addresses harness manufacturing and control as a whole. Its scope excludes RF coaxial cable assemblies and optical-fiber links; specialized operations such as soldering and crimping also remain subject to their respective standards.[7][8][9]
Once the harness is complete, typical checks include point-to-point continuity, interface verification, insulation resistance, dielectric withstand where appropriate, shield continuity and, where needed, circuit resistance. RF, high-speed data and optical-fiber links also need measurements of their respective transmission properties. Test voltage, connection state and any need to isolate sensitive equipment must follow the product and mission documents. One dielectric-withstand procedure cannot be applied indiscriminately to every interface.
Verification then continues at unit or spacecraft level. Functional tests with real or representative loads can compare key parameters before and after vibration, thermal-vacuum and EMC tests. If an intermittent fault appears only after environmental testing, investigation should follow the conductor, termination, connector and attachment points in turn.
7. A Cable-Selection Checklist for Unit and Subsystem Engineers
- Does the line carry power, a low-level measurement, digital data, RF or high voltage?
- Have continuous and transient demands, and worst-temperature voltage drop, loss or transmission performance, been calculated?
- Are conductor material, cross-section, plating and termination compatible?
- Does the insulation suit the voltage, temperature, outgassing, radiation, abrasion and bending environment?
- Do twisting, shielding, impedance, grounding and segregation match the EMC design?
- Have connector contacts, backshells, bend radius and mating clearance been designed together?
- Are the product specification, exact part number, production line, lot and change history traceable?
- Have harness manufacturing controls, continuity and insulation checks, and equipment-level environmental tests been completed?
Conclusion
There is no highest-specification satellite cable independent of its application. Power lines need acceptable voltage drop and heating; measurement lines protect weak signals; digital buses preserve impedance and timing; RF cables control loss and standing waves; and high-voltage or moving lines place greater demands on insulation and mechanical life.
Reliable electrical connections emerge from a continuous chain of evidence: interface requirements, material and construction choices, product specifications, harness manufacturing and spacecraft-level verification. The wire is only one part of that chain.
For teams developing satellite missions, cable and harness decisions need to fit the spacecraft’s wider integration and test plan. STARPATH GLOBAL helps international customers identify competitively priced satellite, payload and assembly, integration and test (AIT) options from China. Teams can contact STARPATH GLOBAL to discuss their technical requirements and explore options suited to their mission and budget.
References
[1] GJB 773B—2015, General Specification for Fluoropolymer-Insulated Wires and Cables for Aerospace Applications.
[2] GB/T 35852—2018, Aircraft General-Purpose Cables and Conductors for Aerospace Applications — Dimensions and Characteristics.
[3] GB/T 42043—2022, Aerospace — Aluminum Alloy and Copper-Clad Aluminum Conductors for Electrical Wires — General Performance Requirements.
[4] GB/T 46556—2025, Classification and Requirements for Application Levels of Space Components.
[5] GB/T 46560—2025, Requirements for Establishing and Implementing a Process Control System for Space Components.
[6] NASA GSFC, EEE-INST-002, Instructions for EEE Parts Selection, Screening, Qualification, and Derating, April 2008, Incorporated Addendum 1, Section W1: Wire and Cable.
[7] NASA-STD-8739.4A with Change 4, Crimping, Interconnecting Cables, Harnesses, and Wiring.
[8] ECSS-Q-ST-70-26C Rev.1 Corr.1, Crimping of High-Reliability Electrical Connections, 2017.
[9] ECSS-Q-ST-20-30C, Manufacturing and Control of Electrical Harness, 2025.
[10] ECSS-E-ST-20-07C Rev.2, Electromagnetic Compatibility, 2022.
[11] ECSS-E-ST-50-12C Rev.1, SpaceWire — Links, Nodes, Routers and Networks, 2019.
[12] NASA-HDBK-4007A, Spacecraft High-Voltage Paschen and Corona Design Handbook, 2026.
[13] ECSS-E-ST-20-01C, Multipactor Design and Test, 2020.
[14] NASA GSFC-STD-8011, Cuprous Oxide Wiring Contamination (Red Plague) Control Plan, 2024.
[15] Zhu Xiaojie, Gu Yongkun, Feng Yanjun et al., “Detailed Three-Dimensional Design of Satellite Harnesses and Three-Dimensional Production Implementation,” Aerospace Manufacturing Technology, No. 2, 2024, pp. 75–78.
[16] Wang Lei, Jiang Shuo, Sheng Beifei et al., “Lightweight Design and Application of Harnesses for a GEO Communications Satellite,” Aerospace Manufacturing Technology, No. 2, 2022, pp. 27–32.